Hey everyone, it’s Jake from the plunger pump team—today we’re diving into something that gets brought up every single week when customers hit us up: the corrosion resistance of our plunger pumps. Let’s cut the jargon, no fancy textbook garbage, just real talk from a supplier who’s been fixing pumps and helping clients pick the right gear for over a decade. Plunger Pump
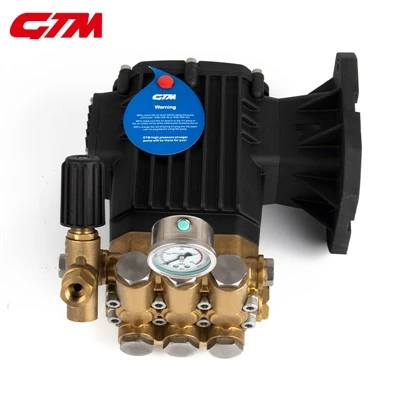
First off—what even is corrosion resistance for a plunger pump, anyway? I see a lot of folks mixing up “it doesn’t rust” with “it’ll last 20 years in my sewage line,” and that’s where things go sideways. Corrosion isn’t just rust, right? It’s when a material reacts with whatever’s flowing through your pump—chemicals, salt, slurries, even just regular old tap water that’s a little acidic. For plunger pumps specifically, the parts taking the brunt are the plungers, cylinders, seals, and valve bodies. Mess that up, and you’re looking at leaks, downtime, replacement parts every few months—total headache.
Let’s start with the core of our pumps, because that’s where most of the resistance happens. We don’t use cheap cast iron that’ll rust through in a year (we’ve had customers bring those back, trust me). Our standard workhorse pumps get treated with what’s called quenched and tempered carbon steel, then coated with a thick ceramic-based enamel that bonds way better than basic paint. Wait, but that’s just the base—when your flow isn’t boring water, like if you’re pumping brine from an oil rig, or acidic cleaning chemicals for a food plant? We step up to 316 stainless steel plungers and cylinders. 316 isn’t just the fancy stainless your friend uses for a grill— it has molybdenum in it, which makes it way better at fighting chloride corrosion. That’s the stuff that eats regular stainless steel alive, like if you’re pumping seawater or road salt runoff.
I remember a client a couple years back—they ran a fish processing plant in Maine, pumping saltwater to chill their processing lines. Swore up and down a competitor’s pump would only last 6 months. They swapped to our 316 stainless plunger pump set, and it’s still running strong 4 years later. No leaks, no pitting, nothing. That’s the stuff that makes us feel good.
But wait—corrosion isn’t just about the metal parts. Seals and packing are huge too, and most suppliers skip this. If your seal breaks down because of the chemicals you’re pumping, even the hardest metal plunger is useless. We don’t use generic rubber seals that turn to mush when hit with caustic soda. We have seals made from EPDM, Viton, even PTFE depending on the fluid. Viton’s for high-acid stuff, PTFE for super caustic or high-temperature fluids—we tailor that to whatever the job needs. Last month we had a battery recycling client pumping lithium-ion slurry, which is super corrosive. We swapped their standard seals for custom PTFE ones, and they haven’t had a seal failure in 8 months, compared to every 6 weeks with their old pump setup. That’s the difference between paying $500 for a pump once and $10k in downtime a year because of bad corrosion.
Now, let’s get real—nothing is completely corrosion resistant. Even 316 stainless will corrode if you push it too far. I’ve seen clients try to pump concentrated sulfuric acid with a standard 316 pump, and wonder why it ate through the plunger in 2 weeks. That’s why we always ask the same 5 questions when someone reaches out: What’s the fluid you’re pumping? What’s its pH level? Temperature? Pressure? And is there anything else mixed in—like solids, salts, chemicals? That’s how we match the right materials, not just throw a “corrosion resistant” label on a pump and call it a day.
We also do a lot of testing in-house, by the way. Not just lab tests—we field test pumps in actual working environments. Last year we ran a test batch of pumps at a municipal wastewater treatment plant that handles industrial runoff, including all kinds of weird chemicals and heavy metals. We set up 6 different pumps, each with different material setups, and checked them every 3 months for pitting, leaks, performance drop-off. The 316 stainless with custom Viton seals came out on top by a mile, outlasting all the others by 2x. That’s data, not guesswork. A lot of suppliers say “our pump is corrosion resistant” with no proof—we show you the test sheets.
Another big one: galvanic corrosion. That’s when two different metals touch each other and cause one to corrode way faster, like putting a steel bolt next to a copper pipe. We design our pumps to avoid that. For example, if the cylinder is 316 stainless, we don’t use a steel fastener to hold it on—we use 316 bolts too, or even plastic fasteners for some low-pressure setups. Small thing, but it’s saved us from so many premature failures. I heard a story from a mining client once that had their pump’s valve body corrode because they used a cheap steel bolt to attach it, reacting with the stainless body. Total waste, all because of a $0.50 bolt. We never cut corners like that.
Now, let’s talk about maintenance, because even the most corrosion-resistant pump will fail if you don’t take care of it. Here’s a tip that we give every customer for free: flush your pump with clean water after every use, especially if you’re pumping chemicals or slurry. That’s it. Most of the corrosion that happens between overhauls is from residual fluid sitting in the pump, reacting with the metal. A 2-minute flush keeps that from happening. We’ve had a customer who forgot that, pumping molasses, and after a month the residual molasses (which is acidic) ate through the plunger seal. He started flushing, and hasn’t had an issue in a year. Simple stuff, but it works.
Wait, what about high-pressure applications? A lot of plunger pumps are used for pressure washing, hydrotesting, oil and gas extraction. High pressure means the plunger is moving back and forth super fast, so corrosion here is even worse because the fluid is constantly abrading the metal too. We use hard chrome plating on plungers for high-pressure standard, but if you’re pumping corrosive fluid, we switch to ceramic coating or even solid tungsten carbide plungers. Tungsten carbide is like, way harder than steel, so it fights both corrosion and abrasion. We had an oil rig client pumping fracking fluid, which is super high pressure and full of chemicals and sand. Their old pump plungers would pit so bad they’d have to replace them every 2 months. We put solid tungsten carbide plungers in, and now they replace them once a year. That’s a massive cost savings for them.
I know a lot of you are wondering: “how long will my pump actually last in my specific application?” The honest answer is: it depends. If you’re pumping regular water, our standard corrosion-resistant pump setup will last 10-15 years, maybe more if you do basic maintenance. If you’re pumping highly corrosive chemicals, like concentrated hydrochloric acid, we can use Hastelloy parts, which is super expensive but will last 5+ years in that stuff. There’s no one-size-fits-all, and we never pretend there is.
Here’s the thing that sets us apart from other plunger pump suppliers: we don’t just sell a pump and ghost you. We talk to you about your specific conditions, not just a generic sales pitch. If you tell me you’re pumping something weird that I’ve never heard of, I’ll go test it, or point you to a setup that’s worked for similar jobs. A lot of big pump companies will just push their “top of the line” pump even if it’s way more expensive than you need. We’re here to get you a pump that works for your budget and your corrosion needs, not just make a sale.
I get it—buying a plunger pump is a big investment, especially when you’re worried about downtime. A broken pump can shut down an entire plant, cost you thousands in lost production. That’s why getting the corrosion resistance right isn’t just a spec—it’s about keeping your operation running smoothly. We’ve had customers tell us that switching to our corrosion-matched pumps cut their maintenance costs by 70% and downtime by 80%. That’s the real win here, not just a pump that doesn’t rust.
If you’re dealing with a corrosive fluid, or you’re tired of replacing pumps every few months because of corrosion, hit us up. We can walk you through the material options, send you test data, even help you spec out the right pump for your exact job. No pushy sales calls, no vague “this is the best” lines—just real answers from people who work with plunger pumps every single day. We’ve helped everyone from small factories to big municipal plants, and we’re happy to help you too.
High Pressure Washer Accessories References
- ASM International. (2020). Corrosion of Metallic Materials. ASM Handbook, Volume 13A: Corrosion: Fundamentals, Testing, and Protection.
- Shreir, L. L., Jarman, R. A., & Burstein, G. T. (Eds.). (2010). Corrosion: Volume 1, 4th edition. Elsevier.
- NACE International. (2018). Materials Selection for Corrosion Control. NACE International Standard SP0178.
- Plunger Pump Design and Application Guide. (2022). Hydraulic Institute.
Zhejiang GTM Hi-Tech Intelligent Equipment Co., Ltd.
We are one of the most experienced plunger pump manufacturers and suppliers in China, also support customized service. Please feel free to buy discount plunger pump for sale here from our factory. Quality products and reasonable price are available.
Address: No.5 of Changjiang Road, 2nd Economic Development Zone of Wenling, Zhejiang, China
E-mail: yehuanting1@hongyemfg.com
WebSite: https://www.gtmplungerpump.com/
